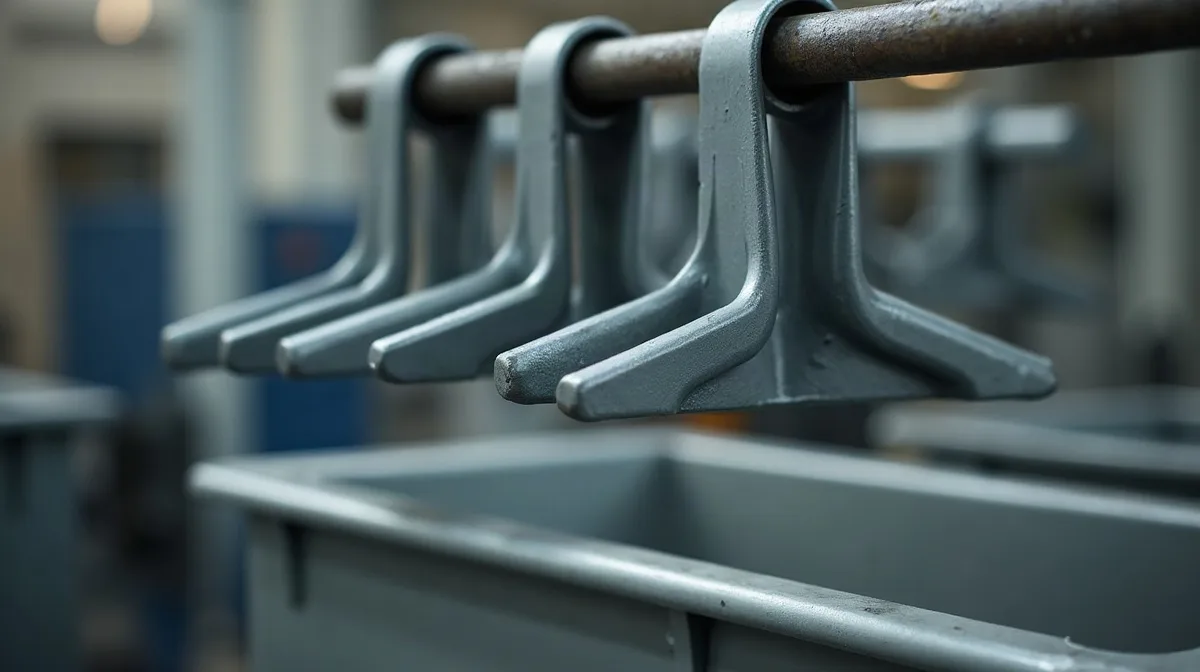
Paint that peels after one winter, powder coating that blisters along the edges, a bolt that seizes the first time it is tightened: in many workshops the cause is not the topcoat but what happened to the metal before it. Phosphating is one of the oldest and most widely used ways to prepare steel for what comes next, yet the choice between its main types is often made by habit rather than by need. This guide walks through how the process works and how to match the coating to the job.
What a phosphate conversion coating actually is
Phosphating is a conversion coating, applied mainly to steel or iron as a pretreatment before another form of corrosion protection. A dilute solution reacts with the metal and turns its surface into a layer of microscopic phosphate crystals, typically containing iron, zinc or manganese. Because the layer grows out of the metal itself instead of being laid on top of it, it bonds tightly and gives paint, oil or wax a textured surface to grip.
The crystalline structure is the key. It increases the surface area of the substrate, which is a large part of why phosphate layers improve paint adhesion. It also holds oils and waxes, which matters for parts that are oiled rather than painted.
The three main types and where each fits
- Iron phosphate improves paint adhesion and impact resistance and gives some protection against oxidation. It is inexpensive, appears pale blue to grey, and offers the least corrosion resistance of the three, so it is mostly used on equipment that stays indoors.
- Zinc phosphate is the usual choice when ferrous parts face harsh weather and corrosion is the main concern. It is popular in the automotive industry, works on mixed metals such as steel, galvanised steel and aluminium, and can be dyed to a matte black finish.
- Manganese phosphate is used mainly as an undercoat for lubricants or paint. It is highly absorbent, carries oils and waxes, and resists wear and galling, which makes it a common finish for moving parts. Its colour is dark grey to almost black.
In short: iron phosphate for simple paint preparation on indoor parts, zinc phosphate for outdoor durability, manganese phosphate for friction and wear.
A typical process line, step by step
Whatever the chemistry, the sequence follows the same logic: cleaning, rinsing, surface activation, phosphating, rinsing, an optional neutralising rinse, and drying. Iron phosphate lines usually run in two to six stages and can be applied by immersion or spray, so pretreatment can run continuously with the paint line. Zinc phosphate needs more stages because it requires a surface conditioning step before the phosphate bath.
Cleaning is where most failures begin. If soils remain on the surface, the conversion coating does not form evenly and corrosion protection suffers. Alkaline cleaners deal with organic soils such as oils, while acid cleaners remove inorganic soils such as oxides. Rinses then stop the chemical reactions, remove leftover chemicals and limit carryover from one tank to the next.
For smaller operations, products that combine several of these steps can simplify the line. Suppliers of industrial phosphate coatings offer, for example, liquids that derust, clean and phosphate in a single step, low-temperature iron phosphates for dipping or spraying, microcrystalline zinc phosphates for paint bonding and corrosion protection, and heavy manganese coatings for moving parts that will be oiled or painted.
Sealing and post-treatment
A phosphate layer on its own is porous. Post-treatments after conversion coating improve corrosion and humidity resistance. Chrome-based seals have largely given way to trivalent chrome, non-chrome and polymeric dry-in-place options. Iron phosphate processes usually finish with a sealer, often amine or nitrate based, while zirconium-based sealers are gaining ground because they improve adhesion further. If the parts go on to electrocoating, the line needs a final deionised or reverse osmosis rinse, and the seal must survive that rinse.
Checking that the coating is right
Three characteristics define a conversion coating: coating weight, crystal structure and chemical composition. Crystal structure is checked by optical or scanning electron microscopy, and composition in a laboratory. Day to day, visual inspection is still useful. Shiny spots on a part that should be uniformly grey usually mean that no phosphate formed there, a sign that the surface was contaminated and the cleaning stage needs attention. Streaking can point to misaligned spray nozzles or uneven pressure.
Choosing for your parts
Start with where the part will live and what it must do. Indoor cabinets, shelving and enclosures that will be painted rarely need more than a well-run iron phosphate line. Parts exposed to weather, road salt or humidity justify the extra stages of zinc phosphate. Gears, fasteners and sliding components that will be oiled benefit from manganese phosphate. Keep in mind that phosphating is typically applied to carbon steel, low-alloy steel and cast iron, so other substrates may call for a different pretreatment altogether. Get the cleaning right, choose the type that matches the service conditions, seal where needed, and the topcoat will have a sound base to build on.
Sources
- Corrosionpedia, What Does Phosphating Mean?. https://corrosionpedia.com/definition/phosphating
- Hubbard-Hall, What are the benefits of iron phosphates compared to zinc and manganese phosphates?. https://www.hubbardhall.com/proof/knowledge-center/what-are-benefits-iron-phosphates-compared-zinc-and-manganese-phosphates
- Products Finishing, Pretreatment for Painting. https://pfonline.com/articles/pretreatment-for-painting
Διαβάστε επίσης
 ΤεχνολογίαΠρόγραμμα διαχείρισης αποθήκης: τα κριτήρια επιλογήςBarcode, θέσεις, picking, φορητές συσκευές και σύνδεση με ERP και e-shop: τι να ελέγξετε πριν επιλέξετε σύστημα για την αποθήκη σας.17/11/2026 · 5 λεπτά ανάγνωσης
 ΤεχνολογίαΕσωτερικοί σύνδεσμοι: ο σκελετός της προώθησης με SEOΟι σύνδεσμοι ανάμεσα στις σελίδες ενός site καθορίζουν τι θα βρει η Google και πώς θα κινηθεί ο επισκέπτης. Τι προτείνει η ίδια η Google για anchor text, ιεραρχία, breadcrumbs και sitemap.27/10/2026 · 5 λεπτά ανάγνωσης
 ΕκδηλώσειςΤο νυφικό κρεβάτι στην ελληνική παράδοση και πώς το ετοιμάζετεΠώς γίνεται το στρώσιμο του νυφικού κρεβατιού, τι συμβολίζουν το ρύζι και τα χρήματα και πώς διαλέγετε σεντόνια και σετ για εκείνη τη μέρα.19/11/2026 · 5 λεπτά ανάγνωσης
Κάτι δεν στέκει;
Αν κάποιο στοιχείο έχει αλλάξει ή είναι ανακριβές, στείλτε μας τη διόρθωση και θα ενημερώσουμε το κείμενο.